
Industry: Aggregates
Application: Air Handling Fans
Site Challenge:
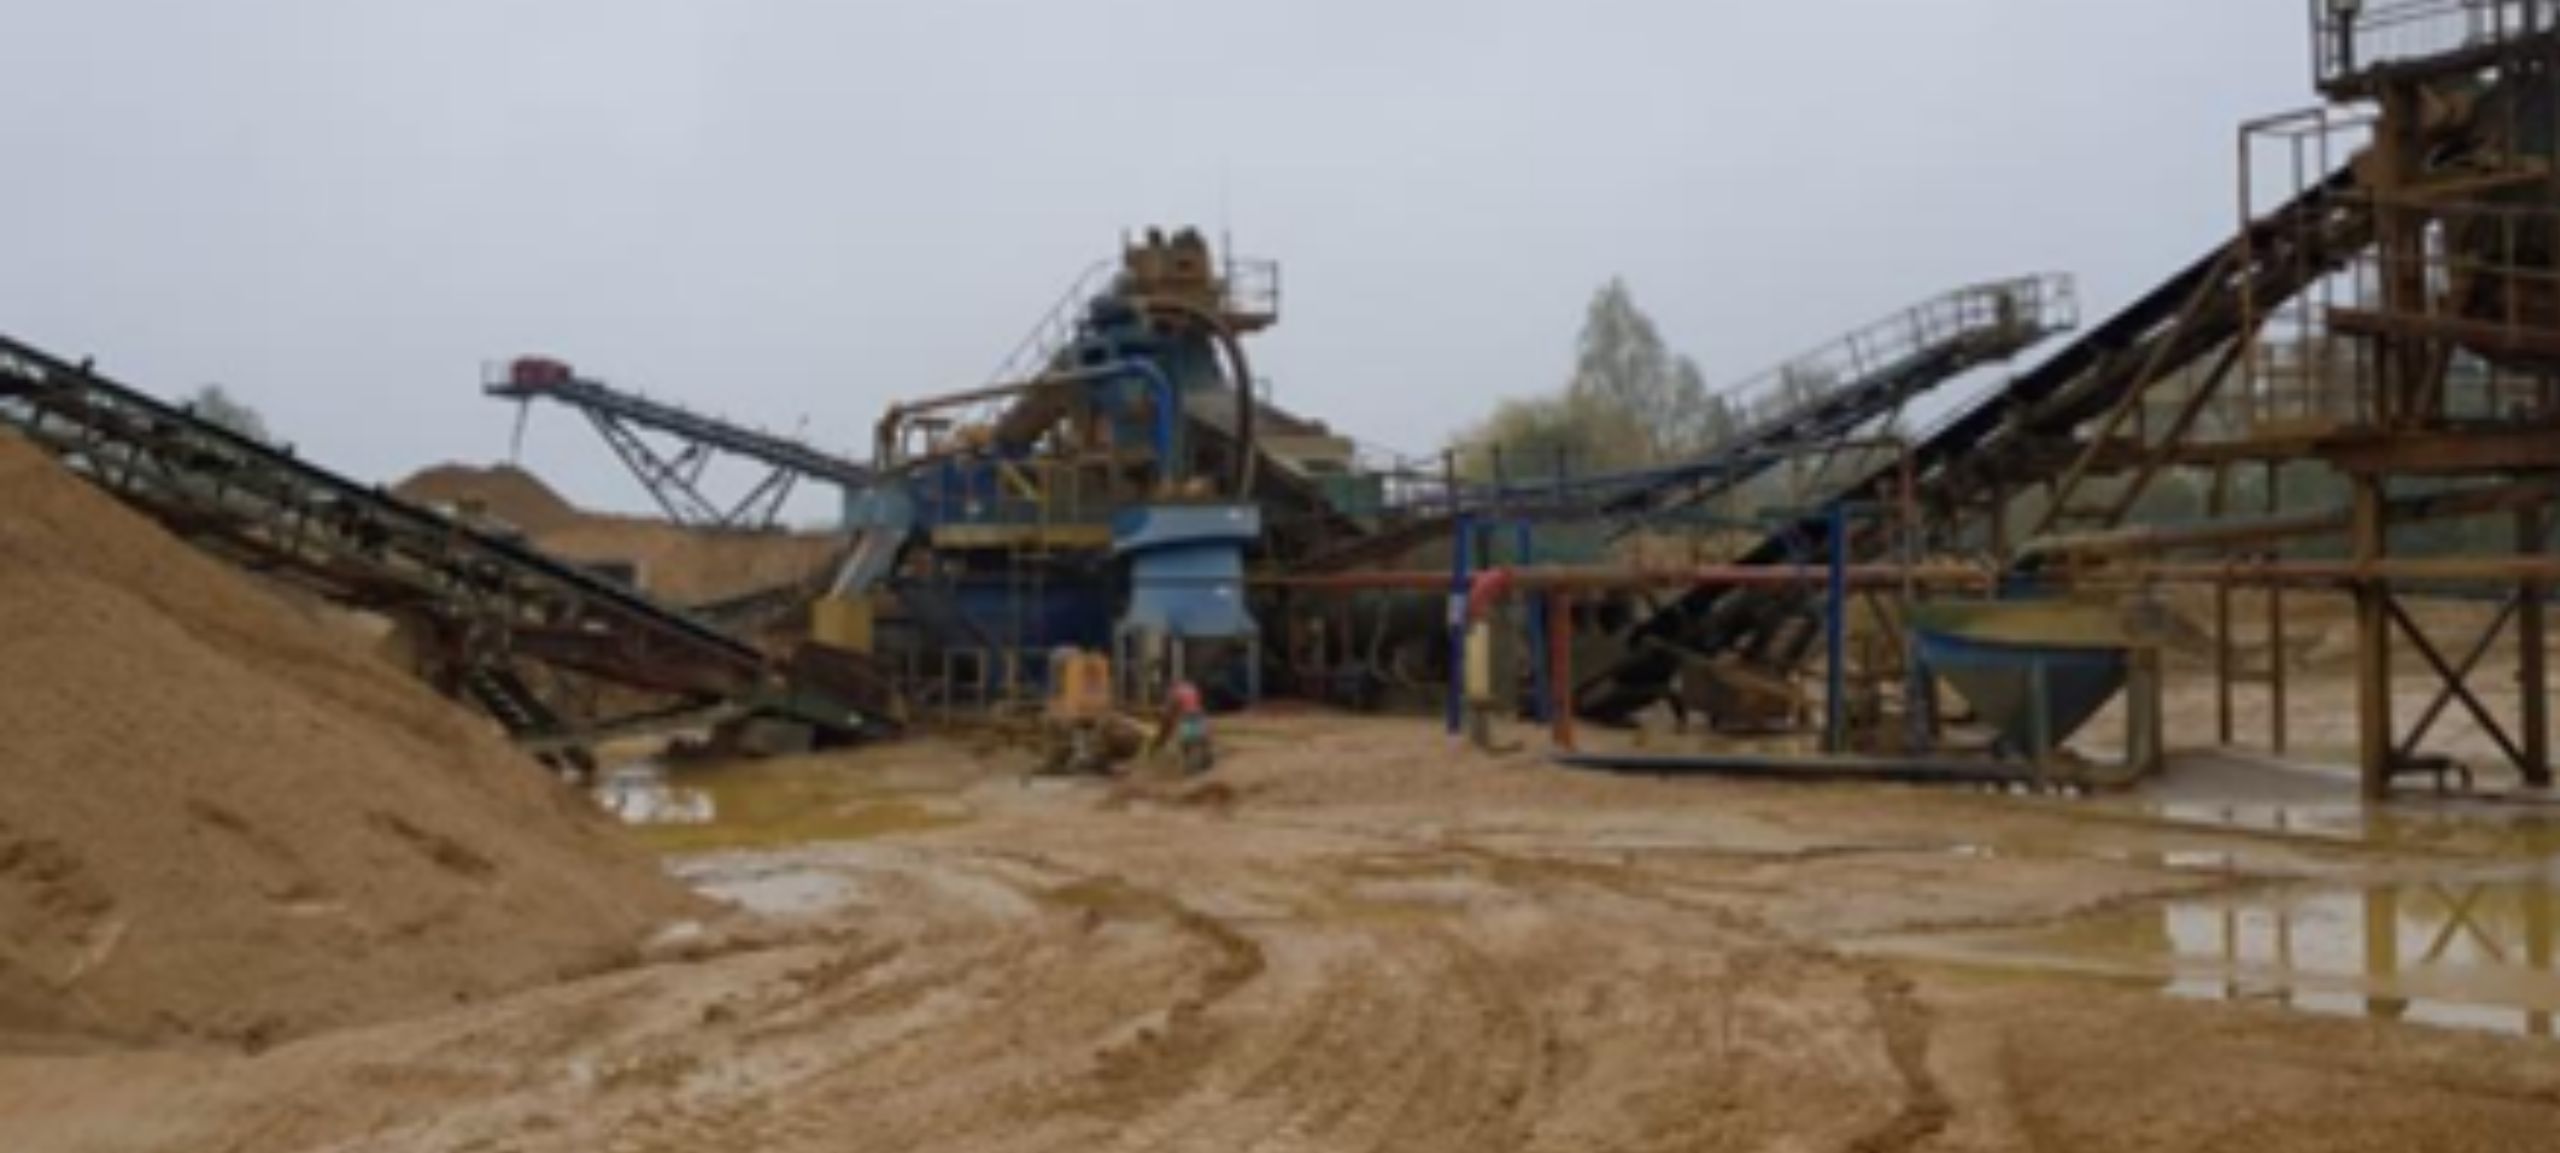
Aggregate production at Hills Quarry Products’ Cerney Wick site in Gloucestershire demands a high volume of water which returns to a sump for pumping to a settling bed. Float level switches in the sump activate a fixed speed pump.
However, the fixed speed could be too high for demand, leading to the sump running dry and the pump failing. In addition, because the motor only runs at one speed, the stress on the pump set could lead to broken transmission belts, motor overcurrent or blocked pumps, leading to costly failures, typically every two weeks.
“The pump could be out of action for a few hours to a full day, depending on if it was a simple belt change or if the pump needed to be raised from the sump,” says Olly Thompson, Quarry Manager. “We extract between 1,000 and 1,200 tonnes of aggregate every day at Cerney Wick, so any downtime is extremely costly – not just in terms of lost production, but also due to the extra expenses incurred by our maintenance team and external contractors.”
APDS Solution:
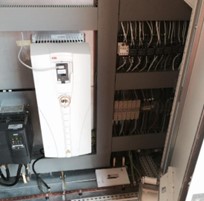 APDS were asked to investigate. APDS recommended, a 55 kilowatt (kW) variable speed drive along with a local level control device. These were installed to automatically adjust the pump motor’s speed according to demand. A pressure transducer, installed in the sump, monitors water pressure.
The VSD then calculates the water level that corresponds to this measured pressure, adjusting the pump speed to avoid overflows or the sump running dry.
“This system has reduced downtime, increased production and reduced the number of replacement drive belts as well as the cost of repairing the pump when it ran dry,” says Thompson. “As well as avoiding failures and the associated costs, we have also cut electricity usage on the application by around 50 percent by matching motor speed to demand, achieving further savings.”
Benefits:
- Up to 1,200 tonnes of aggregate per day can now be consistently extracted by avoiding pump failures following the conversion of a fixed speed motor to variable speed control.
- Automatic Control System
- Minimised breakdowns
- Less maintenance
- 50% Reduction in energy costs
Conclusion:
Hills Quarry Products has reduced pump failures and cut maintenance and energy costs using an ABB variable speed drive. Up to 1,200 tonnes of aggregate per day can now be consistently extracted by avoiding pump failures following the conversion of a fixed speed motor to variable speed control.
“This system has reduced downtime, increased production and reduced the number of replacement drive belts as well as the cost of repairing the pump when it ran dry,” says Thompson. “As well as avoiding failures and the associated costs, we have also cut electricity usage on the application by around 50 percent by matching motor speed to demand, achieving further savings.”
Footnote:
Please note these customer-approved stories are collected since 2000. While some company names may have changed during this time, the principles and methods described to save energy or improve productivity are applicable today. contact APDS Ltd Bristol: 01179 822 049 www.apds.co.uk
Have a similar project or application? Why not contact us to discuss your needs?